
In industries such as pharmaceuticals, food, chemicals, and materials, powder mixing is an extremely common yet critical process. Whether producing a single pill, a packet of infant formula, or a batch of ceramic powders or battery materials, the uniformity of the mixture directly affects the quality, performance, and safety of the final product. However, one of the most common questions during the mixing process is: How do I know when the powders are thoroughly mixed?
Many people rely on experience: “It looks like the same color now” or “It’s been stirred for ten minutes, so it should be good enough.” However, in industrial production and laboratory research, such subjective judgments are far from sufficient. The endpoint of powder mixing cannot be determined by visual inspection alone; it requires scientific methods for verification.
I. Why “Looking Uniform” Does Not Equate to True Uniformity
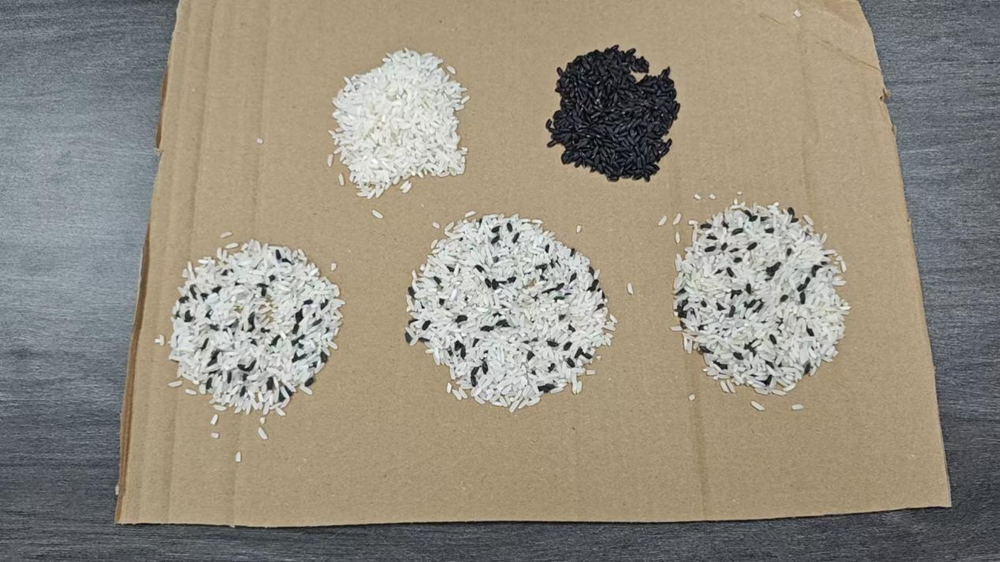
Powders are systems composed of a large number of microscopic particles. Particles of different components often vary in particle size, density, shape, and surface properties. During the mixing process, particles are subject to two opposing forces: convection, diffusion, and shear cause them to intermingle, while gravity, electrostatic forces, and agglomeration may cause them to segregate again.
Therefore, even if the surface appears uniform in color, localized enrichment or depletion may still exist internally.
II. The Core Metric for Assessing Mixing Uniformity
To scientifically determine whether a powder is uniformly mixed, we must first clarify a key concept: mixing uniformity. It is typically measured using statistical indicators, the most common of which is the relative standard deviation (RSD).
The specific procedure involves taking multiple samples from different locations within the mixing equipment (such as top, middle, bottom, left, right, front, and back), then testing the concentration of a key component (usually the component with the lowest content or the most important one) in each sample. The RSD is calculated by determining the mean and standard deviation of these concentrations and then dividing the standard deviation by the mean.
Generally speaking, the lower the RSD, the closer the concentrations are across the various points, indicating a more uniform mixture. Acceptable RSD standards vary by industry: the pharmaceutical industry often requires an RSD of less than 5%, while the food and chemical industries may allow for a higher threshold of around 10%. However, specific standards depend on product requirements and regulatory provisions.
III. Logic for Determining the Mixing End Point
Determining whether mixing is complete cannot be based on a single point in time. The standard practice is to take multiple samples at regular intervals during the mixing process and calculate the RSD. When the RSD falls below the acceptable standard, and continued mixing no longer results in a significant decrease in RSD—or even causes it to rise again due to overmixing—the mixing end point is considered to have been reached.
Important Reminder: Longer mixing times are not necessarily better. Overmixing can lead to particle breakage, increased static electricity, and component separation, which actually compromises uniformity. Therefore, determining the optimal mixing time is a critical step in process development.
IV. Common Factors Affecting Mixing Uniformity
Even with the correct method, mixing results are still influenced by various factors:
- Differences in particle size and density: The greater the difference, the more likely stratification will occur.
- Particle shape and surface properties: Spherical, smooth particles have good flowability but may be harder to retain; irregular particles are prone to agglomeration.
- Moisture Content and Static Electricity: Moisture or static electricity can exacerbate agglomeration and impair dispersion.
- Mixer Type and Rotational Speed: V-blenders, twin-cone mixers, ribbon mixers, and other types each have their own suitable applications.
- Load Volume: Both excessive and insufficient loads can reduce mixing efficiency.
Therefore, when determining the end point of mixing, one must consider the specific material and equipment conditions; standard procedures cannot be applied blindly.
Post time: Sep-24-2026